A factory's quality promise, or a PDF of a system certificate, is not a check of the packed lot you are about to ship. A third-party pre-shipment inspection (PSI) is an independent examination of a particular order, usually at the factory just before dispatch, against your written specification or approved sample. This guide is for importers, wholesalers, garment factories and brand buyers of safety pins and other small metal garment accessories from India.
It complements our sample evaluation checklist, the quality-control buying guide and the article on checking a supplier's certificates. The question here is narrower: once you have approved a sample and placed an order, how do you book a third-party inspection, what should the inspector check on safety pins, how does AQL sampling under ISO 2859-1 work, who pays, and what should the report contain?
This is general buyer guidance, not legal, customs or laboratory advice, and it is not a statement that any named manufacturer holds ISO 9001 or any other certificate, or that any named inspection firm is recommended. Official sources below were fetched on 11 November 2026. Agree the inspection rules in the purchase order, and confirm laboratory or market-access tests with your compliance adviser.
Quick answer
A PSI is a lot inspection, not a factory certificate. It does not replace sample approval, a quality-management certificate, or your own check when the goods arrive.
Agree the rules before production: who appoints the firm, when the visit happens, what will be checked, the sampling and pass/fail rule, and what happens if the lot fails.
Sampling is usually by attributes under [ISO 2859-1:2026](https://www.iso.org/standard/2859-1), which replaced the 1999 edition in January 2026. ISO describes AQL (Acceptance Quality Limit) as the maximum average percentage of defective items considered acceptable during random sampling, and uses it to set sample sizes and accept/reject numbers. Confirm which edition the firm will apply.
Typical on-site checks are dimensions and wire diameter, point sharpness and alignment, spring and clasp function, coating or plating and appearance, packing, labels, shipping marks, and counts. Nickel-release and salt-spray evidence, if you need them, are laboratory tests.
Inspect only when the lot is ready, and book in advance. Readiness rules differ by firm (see below). Leave time after the visit for the report and any remedy.
Who pays is a contract point, not a universal rule. Write it into the purchase order. A private quality inspection is not government-mandated preshipment inspection under the WTO Agreement on Preshipment Inspection.
The report should identify the order and the lot, include photographs, and record quantity, conformity, function, measurements, packing, marks, labels, and defect counts against the agreed accept/reject numbers.
Minimum order quantity is negotiable and depends on size, finish and packaging. Discuss an inspection plan through the enquiry form or the contact page.
What a third-party inspection is, and what it is not
ISO/IEC 17020:2026 (published March 2026, corrected June 2026) is the current international standard for inspection bodies. It describes inspection as the examination of an item — materials, products, installations, processes or services — and the determination of their conformity with requirements from standards, regulations, contracts or internal specifications. Inspection can cover safety, quality, quantity and fitness for purpose. The standard sets requirements for competence, impartiality and consistent operation, and can be used for accreditation.
Accreditation is not compulsory, but it is a way to check a firm. ILAC explains that ILAC Mutual Recognition Arrangement signatories accredit inspection bodies to ISO/IEC 17020, accept one another's accredited results, and keep a list of the bodies they have accredited. Start with ILAC's signatory search, then confirm status and scope with the accreditation body in the economy where the inspection body is based.
A PSI is not a substitute for approving a sample: keep a sealed reference for the inspector. It is not proof that a factory's quality system is certified: an ISO 9001 certificate, if one is claimed, does not inspect your packed cartons. It is not the same as a mill or fastener inspection document. ISO 16228:2017 covers fastener inspection documents (a declaration of compliance and several test-report types) issued for finished fasteners, including pins, at the purchaser's request. That paperwork describes material or tests for a delivery; a PSI report records how a particular packed lot was checked against your specification. Neither replaces the other.
It is also not government-mandated preshipment inspection. The WTO Agreement on Preshipment Inspection applies to activities contracted or mandated by the government of a "user Member" and defines them as verification of quality, quantity, price (including currency and financial terms) and/or customs classification of goods being exported to that Member's territory. A quality inspection that you appoint as a buyer is a private contract. Do not assume that WTO rules, such as the five-working-day Clean Report of Findings timetable, automatically apply to it.
Use the supplier evaluation checklist when you are still choosing a factory. Use a PSI when you already have an order to protect.
AQL sampling under ISO 2859-1
Most commercial pre-shipment inspections use acceptance sampling by attributes. The inspector draws a random sample from the lot, counts how many items fail the agreed checks, and accepts or rejects the lot (or refers it to you) according to pre-set numbers.
The international standard for that system, used lot by lot and indexed by AQL, is ISO 2859-1. The current edition is ISO 2859-1:2026 (third edition, published 22 January 2026). It replaces ISO 2859-1:1999 and that edition's amendments, which ISO marks as withdrawn. ISO describes the 2026 edition as a system of single, double and multiple sampling plans, with switching rules between normal, tightened and reduced inspection, and skip-lot procedures in this edition.
On AQL, ISO's page for the 2026 standard states that AQL stands for Acceptance Quality Limit, "the maximum average percentage of defective items considered acceptable during random sampling," and that the standard uses the AQL to determine sample sizes and acceptance/rejection thresholds. The official scope, as reproduced on the Swedish Institute for Standards catalogue page for ISO 2859-1:2026, states that the purpose is to incentivize the producer, through the economic and psychological pressure of lot non-acceptance, to maintain a process average at least as good as the specified acceptance quality limit, while providing an upper limit for the risk to the consumer of accepting the occasional poor lot.
AQL is not a licence to ship a fixed percentage of defective pins, and it is not a promise that the uninspected remainder of the lot is defect-free. It is a statistical plan for deciding whether to accept a lot, based on a sample. If the sample is under the rejection number, the lot can still contain defective pieces that were not drawn.
ISO 28590:2017 (confirmed in 2024) introduces the ISO 2859 series. For a continuing series of lots, ISO 2859-1 is the part most commercial firms cite. Confirm the part, the edition and the tables in writing. SGS states that it uses ANSI/ASQ Z1.4 (ISO 2859-1) and produces detailed reports based on a defined AQL. Do not assume that a firm printing "ISO 2859-1" on a booking form has already switched its worksheets from the 1999 tables to the 2026 edition. Ask.
This article does not reproduce the sampling tables. They are in the copyrighted standard, and the right sample size depends on your lot size, inspection level and AQL. Write into the order how a "lot" is defined, the inspection level or scheme, a separate AQL (if you use one) for each defect class you define, with examples for safety pins, and which edition of ISO 2859-1 or ANSI/ASQ Z1.4 the numbers will come from.
There is no official AQL that applies automatically to safety pins. Figures sometimes quoted in trade (for example 2.5 for major defects and 4.0 for minor) are commercial conventions used by some inspection firms, not a requirement of ISO 2859-1 and not a legal limit for this product. Choose levels that match the risk of the defect, and put those levels in the purchase order.
What inspectors check on safety pins
ISO 2859-1 tells you how many pieces to draw and how many defects fail the lot. It does not tell you what a good safety pin is. That list comes from your specification and approved sample. The quality-control buying guide and the sample evaluation checklist set out the product checks in more detail. Put a short version of the same list in the inspection booking.
SGS says a final random inspection covers quality (appearance, performance and workmanship), quantity, packaging, labelling, shipping marks, transportation and drop checks. Bureau Veritas lists quantity, product conformity, workmanship, appearance and function, measurements and on-site tests, packing, shipping marks and labelling. Intertek lists product safety, quantity, workmanship, function, colour, size and packing. For safety pins, specify the following.
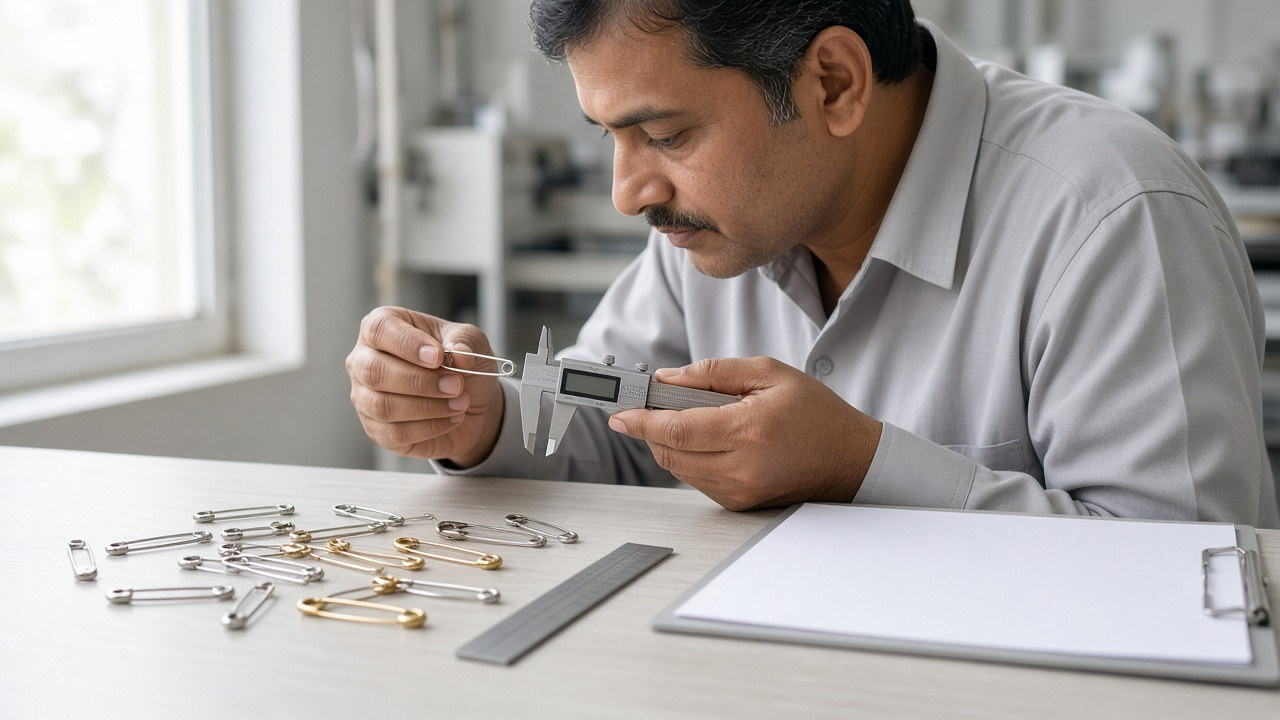
Dimensions and wire diameter. Measure overall length (usually closed) and wire diameter against the millimetre figures and tolerances in your specification, not only against a size number. Check several pieces against the approved reference, and record how and where the pin was measured.
Point sharpness and alignment. The point should be sharp enough to pass through the intended fabric without snagging, free of burrs or a hooked tip, and aligned so that it enters the clasp cleanly. There is no single official sharpness test for safety pins that this article can cite, so if the application is demanding, agree a practical method (visual check, seating in the clasp, and, where relevant, a trial on a named fabric). Exposed points can cause injury; say so in the brief.
Spring and clasp function. Open and close pins from the sample. The action should be smooth and consistent, not excessively loose or stiff, and the pin should return to its closed position. The point should seat in the clasp, remain covered when closed, and not spring open under ordinary handling. If your use is more demanding, define that test before production. Variation across the sample is itself a finding.
Coating, plating and appearance. Compare colour, gloss and coverage with the approved sample. Look for uneven plating, flaking, roughness, scratches, discoloration and visible rust spots. The material and finish named on the order should match what is in the boxes. A visual check can catch obvious plating faults; it cannot measure coating thickness or prove how the finish will age.
Nickel release, where it is relevant. This is not a typical same-day factory-floor check. If you sell into the EU, or supply brands that do, the restriction that most often comes up for metal articles used against the skin is Annex XVII entry 27 of REACH. The consolidated text on EUR-Lex, dated 10 October 2024, states that nickel and its compounds shall not be used in post assemblies inserted into pierced parts of the body unless nickel release is less than 0,2 μg/cm²/week, or in articles intended to come into direct and prolonged contact with the skin if nickel release from the parts in such contact is greater than 0,5 μg/cm²/week. The entry gives examples, including jewellery and watch parts, and "rivet buttons, tighteners, rivets, zippers and metal marks, when these are used in garments." Safety pins are not named in that list. The list is introduced with "such as", so it is not closed. Whether a given use is in scope depends on intended use and on whether contact is direct and prolonged. That is a judgement for you and your adviser. For coated articles, including nickel-plated steel pins, the same entry requires that a non-nickel coating keep release at or below 0,5 μg/cm²/week for at least two years of normal use. A Commission Communication of 20 December 2023 (C/2023/1604) publishes the current test-method titles: EN 1811:2023 for articles intended for direct and prolonged skin contact, and EN 12472:2020 for simulating accelerated wear and corrosion on coated items. If that evidence is relevant, commission a laboratory test on the construction you are buying. The inspector can pull identified samples and send them to a laboratory accredited to ISO/IEC 17025:2017. A one-line "nickel-free" statement is not a test report.
Rust and salt spray, if you source that evidence. The inspector can look for visible rust, staining or disrupted plating. A visual check cannot prove corrosion resistance in storage or in a humid climate. If you want a laboratory corrosion test, the usual international method is ISO 9227:2022, Corrosion tests in artificial atmospheres — Salt spray tests (fifth edition, with Amendment 1 in 2024). The official abstract specifies the apparatus, reagents and procedure for the neutral salt spray (NSS), acetic acid salt spray (AASS) and copper-accelerated acetic acid salt spray (CASS) tests. NSS is particularly applicable to metals and their alloys and to metallic coatings, among other finishes. The same abstract states that the standard does not specify the dimensions or types of test specimens, the exposure period for a particular product, or the interpretation of results, and that the methods are not intended for ranking different materials or for predicting long-term corrosion resistance. There is therefore no official "48-hour" or "72-hour" salt-spray requirement for safety pins in ISO 9227 itself. If you want the test, write the method (usually NSS for a metallic coating), the exposure period and the acceptance rule into the order, and have it done in a laboratory. Do not treat a same-day visual pass as a salt-spray pass.
Packing, labels and shipping marks. For distributors and private-label buyers this is often where lots fail. Ask the inspector to check pieces per inner box, inners per carton, carton construction, product protection, printed labels and artwork, barcodes where you use them, and shipping marks against the packing instructions you approved. Bureau Veritas lists packing, shipping marks and labelling as standard report headings, and names marking and labelling among the most frequent non-conformances it sees (across softlines, hardlines and electrical products, not specifically safety pins). SGS includes packaging, labelling, shipping marks and drop checks. If you need a carton drop test, specify the method rather than assuming one will be done.
Counts. Reconcile the number of cartons with the packing list, then check the stated piece count in a sample of inner boxes drawn from different cartons. Confirm that both sides are using the same unit — pieces, dozens, gross or boxes. Quantity is a standard heading on the SGS, Bureau Veritas and Intertek pages cited above. A count check is not a quality check: a full carton of the wrong pin still "counts" correctly.
How to book an inspection
Treat booking as part of the order, not as a last-minute call the week the container is due.
Name the firm in the purchase order, or reserve the right to appoint one. Many buyers prefer to appoint the inspection body themselves. If the supplier proposes a firm, check independence and, if accreditation is claimed, the scope via ILAC.
Send a complete booking file. Typical contents, reflected in Bureau Veritas' order-review examples, are the purchase-order number, product name, quantities and units, the factory name and address, your specification, packing instructions, the approved or "golden" sample, and your AQL and defect list. Bureau Veritas recommends sending reference samples to the factory in a sealed package, for the inspector's attention.
Book early enough for a genuine visit. Bureau Veritas recommends at least 48 hours' notice (and mentions an early-bird discount for bookings 15 days in advance). Intertek states that it can arrange an inspector on site within five working days of receiving the request.
Inspect only when the lot is ready. SGS inspects when 100 per cent of the goods are produced and at least 80 per cent are packed. Intertek says its final random inspection can only begin after production has been completed and packed ready for shipment. Those are firm-specific readiness rules, not a single ISO requirement. Agree the rule in the booking. Bureau Veritas warns that if the inspector arrives at the booked address and the goods are not being manufactured there, the result can be a "visit in vain" report.
Leave time before the ship cut-off. Bureau Veritas suggests a buffer of at least two to three days so the report can be reviewed and problems remedied before shipment.
Tell the supplier, in the order, that access must be given and that the packed goods, packing list and reference sample must be available. Inspection sits alongside the shipping terms: under many FOB contracts the check happens at the factory before the goods are handed to the carrier, but the Incoterm does not, by itself, write the inspection brief.
The RFQ template is a practical place to put the inspection requirement when you first quote the order.
Who pays
There is no single international rule that says the buyer, or the seller, must pay for a commercial pre-shipment inspection of safety pins. Who appoints the firm, who pays for the first visit, and who pays if the lot fails and must be re-inspected, are points for the purchase order.
In the commercial model described on Bureau Veritas' InSpec FAQ, the client books the service and pays through the firm's payment gateway. Many importers therefore budget the first inspection as a buyer cost. That is a common commercial practice, not a legal default. If the lot fails because of a defect the supplier is responsible for, buyers often provide that the supplier pays for the re-inspection; if the inspector is called when the goods are not ready, the wasted visit may fall on whichever party caused the delay. Write those allocations down.
Do not borrow fee rules from government-mandated programmes. The WTO Agreement regulates inspections contracted or mandated by an importing government. It does not set the price of a private quality inspection you book for your own account.
What the report should contain
You are paying for a usable record of one inspection of one lot, not for a marketing PDF. Based on the public descriptions from Bureau Veritas, SGS and Intertek, a complete commercial report should normally include:
Identification of the inspection firm, the inspector or report number, the date and place, the factory, and your purchase-order and product references.
The quantity presented, the quantity sampled, and the sampling rule (standard, edition, inspection level, AQL and accept/reject numbers).
Photographs of the lot, the packing, the marks and labels, measurements being taken, and examples of any defects.
Results for quantity, product conformity against the specification or approved sample, workmanship, appearance and function, on-site measurements and tests, packing, shipping marks, and labelling.
A count of defects by the classes you agreed, set against the accept and reject numbers, and a clear conclusion (for example accepted, failed, or referred to you for a decision).
Any limitation: goods not ready, sample not available, tests that were not done on site, or samples pulled for a laboratory.
Bureau Veritas says the report is usually issued within a few hours of the inspection (factory location time), on the same day. Intertek says it produces a detailed report, with a photographic record, within 24 hours. Build that timing into the buffer before shipment.
Read the report before you release the shipment. If the lot fails, the defect counts and photographs should be enough to decide, under the rule already in the order, whether the goods will be reworked, sorted, rejected, or accepted under a written concession. The quality-claim guide explains how to handle a problem found later; a clear PSI report is part of that evidence trail. A passed report still does not replace a count and a sample check when the goods arrive, because cartons can be damaged or mixed in transit.
What to write in the RFQ and the purchase order
Put the inspection clause in the order, not only in a chat. Starting from the RFQ template, add, as applicable: whether a third-party PSI is required, who appoints the firm, and who pays for the first visit and for any re-inspection; the readiness rule (for example 100 per cent produced and at least 80 per cent packed, or packed complete, as agreed with the firm); the reference sample and where it will be held; the sampling standard and edition (ISO 2859-1:2026 or the edition the firm will actually apply, or ANSI/ASQ Z1.4), the inspection level, and the AQL and defect classes, with examples for safety pins; the on-site checklist (dimensions and wire diameter, point sharpness and alignment, spring and clasp function, coating and appearance, packing, labels, marks and counts); any laboratory tests, such as nickel release to EN 1811:2023 (and EN 12472:2020 for coated pins) or a salt-spray test to ISO 9227 with a stated method and exposure period; what happens if the lot fails, and that the goods should not ship until you have accepted the report or a written concession; and the destination, Incoterms and the usual shipping documents.
Minimum order quantity is negotiable and depends on size, finish and packaging. Confirm the figure with the quotation.
Red flags
None of these always proves a bad supplier, but each is a reason to pause before you pay a deposit or release a shipment.
The supplier refuses a third-party inspection on a first or large order, or will not agree pass/fail rules in the purchase order.
Inspection is offered only after the goods have been sealed in a container, or on the day of sailing, leaving no time to correct a fail.
There is no approved sample, no written specification, and no agreed AQL or defect list.
The "third-party" inspector is the supplier's own staff, or a firm whose claimed accreditation cannot be found in the accreditation body's directory.
The report has no photographs, no sample size, no defect counts, or no purchase-order or lot identification.
You are asked to accept a "100 per cent inspected" claim without records of what was checked.
Laboratory claims such as "nickel-free" or "salt-spray tested" arrive without a method, laboratory, date or article identification.
You are pressured to ship before you have the report.
Frequently asked questions
What is a third-party pre-shipment inspection for safety pins?
It is an independent inspection of a particular order, usually at the factory when the goods are produced and packed, against your specification or approved sample. It is not a factory certificate, and it is not a government-mandated import inspection under the WTO Agreement.
What does AQL mean, and does it allow a percentage of defective pins?
AQL means Acceptance Quality Limit. In ISO 2859-1:2026 it is the index used to choose a sampling plan, not a licence to ship a fixed percentage of defective pins, and a passed sample does not prove that every uninspected pin is good. Agree the AQL, defect classes and edition in the order; there is no official AQL that applies automatically to safety pins.
When should the inspection take place?
When the lot is actually ready, and early enough that a fail can be corrected before the ship cut-off. SGS inspects when 100 per cent of the goods are produced and at least 80 per cent are packed; Intertek begins after production has been completed and packed ready for shipment. Bureau Veritas recommends booking at least 48 hours in advance and leaving at least two to three days before shipment. Agree the readiness rule with the firm you appoint.
Who books the inspection, and who pays?
For a private quality inspection, the buyer often books and pays, and commercial platforms such as Bureau Veritas' InSpec service are set up that way. It is still a contract choice: write into the purchase order who appoints the firm, who pays for the first visit, and who pays for a re-inspection if the lot fails.
Can the inspector do salt-spray or nickel-release testing at the factory?
Not as a same-day on-site result. ISO 9227 salt-spray testing is a laboratory cabinet method, and the standard does not set the exposure period for a given product. Nickel release, where REACH Annex XVII entry 27 is relevant, is tested to EN 1811:2023 and, for coated items, EN 12472:2020. The inspector can pull samples for a laboratory, preferably one accredited to ISO/IEC 17025.
If the lot passes, do I still need to inspect the goods when they arrive?
Yes. A PSI records the lot as it was at the factory on the inspection date. The arrival checklist is for the later check. Keep the PSI report; it is useful evidence if you later have to raise a quality claim.
Agree the inspection before the lot is packed
Write the inspection firm, the sampling rule, the checklist and the fail procedure into the purchase order, book the visit only when the goods are ready, and read the report before the container leaves. If you already know the sizes, material, destination and whether you want a third-party inspection, send an enquiry or use the contact page: sales@safety-pins.com, +91 6293 155 550 (WhatsApp available), head office at G-4 & 5, City Centre, 19, Synagogue Street (Brabourne Road Facing), Kolkata 700001, India. Minimum order quantity is negotiable.
Sources
ISO 2859-1:2026, Sampling procedures for inspection by attributes — Part 1: Sampling schemes indexed by acceptance quality limit (AQL) for lot-by-lot inspection (fetched 11 November 2026; official ISO page retrieved via a browser-class fetch — a direct curl from this environment received a Cloudflare challenge)
ISO 2859-1:1999 (withdrawn, superseded by ISO 2859-1:2026) (fetched 11 November 2026)
Swedish Institute for Standards, catalogue page for ISO 2859-1:2026 (official scope text) (fetched 11 November 2026)
ISO 28590:2017, Introduction to the ISO 2859 series (fetched 11 November 2026; official ISO page retrieved via a browser-class fetch — a direct curl from this environment received a Cloudflare challenge)
ISO/IEC 17020:2026, Conformity assessment — Requirements for bodies performing inspection (fetched 11 November 2026; official ISO page retrieved via a browser-class fetch — a direct curl from this environment received a Cloudflare challenge)
ISO/IEC 17025:2017, General requirements for the competence of testing and calibration laboratories (fetched 11 November 2026)
ISO 9227:2022, Corrosion tests in artificial atmospheres — Salt spray tests (fetched 11 November 2026; official ISO page retrieved via a browser-class fetch — a direct curl from this environment received a Cloudflare challenge)
ISO 16228:2017, Fasteners — Types of inspection documents (fetched 11 November 2026)
ILAC, Accredited Conformity Assessment Bodies (fetched 11 November 2026)
ILAC MRA Signatory Search (fetched 11 November 2026)
SGS, Final Random Inspection (fetched 11 November 2026)
Bureau Veritas CPS, InSpec Frequently Asked Questions (fetched 11 November 2026)
Intertek, Final Random Inspection (FRI) (fetched 11 November 2026)
WTO, Agreement on Preshipment Inspection (fetched 11 November 2026)
Regulation (EC) No 1907/2006 (REACH), consolidated text of 10 October 2024, Annex XVII entry 27 (fetched 11 November 2026)
Commission Communication C/2023/1604 of 20 December 2023, standards under REACH Annex XVII entry 27 (fetched 11 November 2026)
Live Suvik Overseas pages linked in the body, each checked HTTP 200 on 11 November 2026 (see plan-2026-11/day10/linkcheck-2026-11-11.txt)